When we observe the titanium-gold stainless steel cladding panels shimmering in the sunlight on skyscraper facades or feel the delicate jet-black coating on smartphone frames, few realize that these aesthetically and functionally superior surface finishes originate from a "microscale material reconstruction" technology—Physical Vapor Deposition (PVD). Compared to traditional electroplating, PVD requires only a 0.1–1 μm thick film (equivalent to 1/500th the diameter of a human hair) to endow stainless steel with exceptional wear resistance, corrosion resistance, and vivid color. This "transformative power in minuscule dimensions" has made it a core surface treatment technology in modern architectural decoration, high-end home appliances, medical devices, and other fields.
The magic of PVD lies in its ability to create entirely new material properties on stainless steel surfaces through purely physical processes. In a vacuum chamber, atoms from metal targets like titanium and chromium are excited into a plasma state, acquiring "directional flight" capabilities before depositing onto the stainless steel substrate to form thin films. This process not only eliminates cyanide pollution associated with traditional electroplating but also achieves a full color spectrum from golden yellow to jet black through precise control of film composition and structure. This article systematically dissects the underlying principles, key processes, and operational details of this technology, unraveling the materials science behind colored stainless steel sheets.
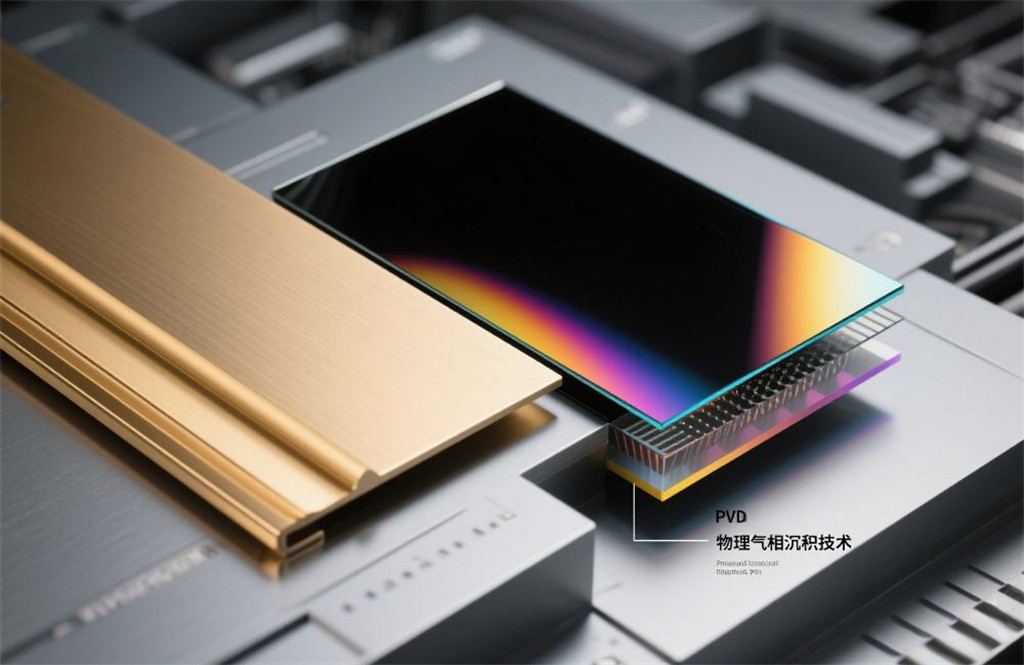
The core of PVD technology is the vapor-phase transfer and deposition of materials through physical means in a vacuum environment. Unlike Chemical Vapor Deposition (CVD), film formation does not involve chemical reaction intermediates; instead, target atoms are transferred to the substrate via evaporation, sputtering, or ionization. For stainless steel coating, this process unfolds in three critical stages:
Vaporization: Target materials (e.g., titanium, zirconium, chromium) are decomposed into atomic or ionic states under high-energy excitation (electron beam bombardment or electric field acceleration).
Transport: Gaseous particles travel freely in a vacuum, guided by electric or magnetic fields toward the stainless steel substrate.
Deposition: Particles adsorb and diffuse on the substrate surface, forming chemical bonds and growing into continuous films.
The vacuum environment (typically below 10⁻³ Pa) is pivotal: it minimizes gas molecule scattering of target particles, ensures deposition precision, and prevents unwanted reactions between metal particles and gases like oxygen.
Stainless steel (commonly grades 304, 316, etc.) serves as an ideal substrate due to its inherent passive oxide layer (Cr₂O₃), which provides a robust adhesion foundation for PVD films. However, achieving high-strength bonding requires ion bombardment cleaning: under a 200–1000V negative high voltage, argon ions (Ar⁺) strike the stainless steel surface at high speeds, not only removing contaminants but also energizing surface atoms to form a diffusion layer (4–5 μm deep) with subsequent target atoms. This "micro-metallurgical bonding" far exceeds the mechanical adhesion strength of conventional coatings.
During film growth, reactive gases can be introduced to form compound films: nitrogen (N₂) reacts with titanium to produce golden titanium nitride (TiN), while methane (CH₄) reacts with chromium to form black chromium carbide (CrC). This reactive PVD (RPVD) enables precise control of film stoichiometry for color 微调 —for example, varying the nitrogen-to-methane ratio can transition titanium-based films from rose gold (TiCN) to dark brown.
The color of PVD films arises from the interplay of two physical effects:
Material Intrinsic Color: Optical properties of metal compounds, e.g., TiN’s golden hue from selective absorption of visible light.
Thin-Film Interference: When film thickness approaches light wavelengths (100–500 nm), reflected light from upper and lower surfaces interferes, creating colors like blue or purple in titanium oxide (TiO₂) films.
In practice, these mechanisms are often combined. For instance, a process might deposit a 50 nm chromium absorption layer followed by an 80 nm silicon oxide (SiO₂) interference layer to achieve deep blue. Spectrometers monitor deposition to maintain color deviation within ΔE < 1 (imperceptible to the human eye).
Pretreatment of stainless steel substrates directly impacts film adhesion, aiming for "atomic-level cleanliness":
Mechanical Polishing: Using No.4 or No.8 mirror finishes to achieve surface roughness Ra < 0.05 μm for uniform deposition.
Ultrasonic Cleaning: 15-minute ultrasonic treatment in 60°C alkaline detergent to remove oils, followed by three 8-minute rinses in deionized water.
Acid Activation: Etching in a nitric-hydrofluoric acid mixture (5:1 v/v) for 30 seconds to remove passive oxide layers and create micro-roughness for enhanced anchoring.
Vacuum Drying: 80°C vacuum drying to prevent recontamination.
Production data shows that water break time (a cleanliness indicator) must exceed 30 seconds; otherwise, adhesion drops by over 40%.
Chamber preparation requires strict control of vacuum levels and leak rates:
Rough Vacuum Pumping: Use roots pumps to reduce pressure to 1 Pa.
Baking Outgassing: Heat to 120°C for 2 hours to remove adsorbed water vapor and organics.
High Vacuum Pumping: Employ turbomolecular pumps to achieve <5×10⁻⁴ Pa, where mean free path of gas molecules exceeds meters.
Leak Test: Pressure rise ≤1×10⁻³ Pa after 30 minutes with pumps off.
Ion Bombardment: Introduce argon to maintain 1–10 Pa pressure, apply 500V negative bias for 5–30 minutes until surface temperature reaches 150°C (enhancing atomic diffusion).
Target Cleaning: Activate target power (5–10 kW) for 2-minute pre-sputtering to remove oxide layers and ensure particle purity.
Example: Magnetron sputtering for rose gold (TiCN) film:
Target: Titanium alloy (Ti90% + Al10%).
Reactive Gases: Nitrogen (50 sccm) + methane (10 sccm), with argon (80 sccm) as carrier gas.
Parameters: 8 kW sputtering power, 100V substrate bias, 180°C temperature, 15-minute deposition (0.5 μm thickness).
Color Control: Optical monitoring adjusts nitrogen flow to maintain target coordinates (e.g., L*=75, a*=15, b*=20).
For large sheets (e.g., 1219×2438 mm), multi-target symmetrical layouts ensure ≤5% thickness uniformity. Planetary workpiece rotation (5 rpm) improves coating consistency on complex shapes.
Environmental Friendliness: No cyanide or heavy metal wastewater; compliant with EU RoHS and REACH.
Superior Performance: Film hardness up to 2000 HV (5× stainless steel), friction coefficient as low as 0.2, 3–4× longer lifespan than electroplating.
Design Freedom: Over 20 standard colors (gold, black, blue) with customizable options for architectural personalization.
Color Drift: Mitigated via gas flow-color models for closed-loop control.
Film Pinholes: Reduced by regular molecular pump oil/filter replacements to <1% defect rate (ISO 21874).
Edge Effect: Enhanced edge deposition via pulsed bias (10–50 kHz) for complex geometries.
Colored stainless steel sheets are widely used in:
Architectural Decoration: Facades, elevator panels, handrails (5000+ hours weather resistance).
High-End Appliances: Refrigerator doors, range hoods (200°C heat resistance).
Medical Devices: Surgical instrument casings (3000+ alcohol wipes without fading).
Future Directions:
Low-Temperature Processes: <100°C deposition for thermosensitive substrates like plastics.
Multi-Functional Integration: Combining with DLC (diamond-like carbon) for superhydrophobic or antibacterial properties.
Smart Coating: AI vision systems for real-time color/thickness adaptation.
PVD vacuum coating redefines stainless steel’s surface potential through nanoscale precision control of material growth. From plasma excitation of target atoms to color precision, every step embodies the synergy of materials science and engineering. As environmental demands grow and design needs diversify, this "vacuum alchemy" will continue to expand into new frontiers, redefining the possibilities of metal surfaces. For manufacturers, mastering PVD’s core parameters and control logic is not only critical for quality assurance but also a key competitive edge in the high-end surface treatment market.


